Contract Assembly Manufacturers - India

MECHANICAL ASSEMBLY MANUFACTURERS FROM INDIA

Castings, forgings, CNC parts, stampings, rubber, and fasteners built into one tested unit. Torque logged on every critical joint, leak tested per serial, packed to your line. One accountable team from drawing to your US dock. India first, more regions as your volume grows.

Assembly volume runs through India today. We program-manage in Mexico and Vietnam too, when buyers need a multi region resilience plan.
38+
Parts in 1 Build
Castings, forgings, CNC, rubber, fasteners
13
Sub Suppliers, 1 PO
Managed on a single assembly
5
Functional Tests
Leak - torque - pressure decay
7 Weeks
Critical Sample
Built across 13 partner floors
IATF 16949 ISO 9001 ISO 14001 ISO 45001 PPAP Level 3 ISO 2768 VDA 6.3 ASTM B117 ISO 9227 AIAG SPC AIAG MSA RoHS REACH
Our Assembly Partners' Certifications
At a glance

VIA INDIGOS is a US contract manufacturing company that runs mechanical assembly programs in India, as one accountable team from drawing to US dock. Child part sourcing, kitting, assembly, torque control, functional testing, and packing sit under one program, with PPAP Level 3 at the assembly level.

Scope
Full assemblies, sub assemblies, kitted child parts, and electro mechanical box builds, with torque control and functional testing
Network
Assembly benches in 6 Indian cities, drawing child parts from a 470+ facility network spanning 22+ cities
BOM depth
Builds up to 38+ parts, 7 processes, and 13 sub suppliers on one PO
Torque control
DC torque tools on every critical joint, values logged per serial, calibration certificates on file
Quality
PPAP Level 3 at assembly level, IATF 16949 and ISO 9001 partners, child part PPAPs rolled in
Testing
Pressure decay, hydraulic leak, vacuum function, and endurance cycling, recorded per serial
Built for
US buyers with recurring volume who want 1 PO for the whole build, not 13
Accountability
One named person from RFQ to delivered parts

The procurement emails
you already know.

60%
Of your week goes to chasing sub suppliers

If you have ever sourced a multi part assembly from anywhere in the world, you know the routine. Email at 9 in the morning. No reply. Email again at 4. Maybe an answer Tuesday. We built VIA INDIGOS so the fifth email never lands. Because on an assembly, one late child part strands every finished part on the bench with it.

Procurement Inbox · Tuesday 9:47 AM
142 unread
Spring supplier slipped 11 days - 26 parts sitting done 19 The detent spring lot is still at heat treat. The other 26 parts of the gearbox build are inspected and on the bench. Nothing can close, and my line goes down Thursday. 9:47 AM 4 of 50 pump assemblies failed leak at 6 bar 16 Pressure decay caught 4 units losing 12 mbar in 30 seconds against a 4 mbar limit. Vessel cutoff is in 3 days and nobody can tell me if it is the O ring lot or casting porosity. Yesterday M8x1.25 bolts arrived for M8x1.0 tapped housings 11 The fastener supplier shipped coarse thread against the BOM. 8,000 bolts are useless and the housings are tapped fine. Who owned the BOM revision when the drawing changed? Mar 14 No torque records - warranty claim lands on us 14 The customer returned 60 units with loose cover bolts. The shop swears they torqued to spec, but there is no torque log for the lot, so we are eating the claim and the freight. Mar 8 Foundry and machine shop blaming each other 23 The machining shop says the casting is oversize on the datum face. The foundry says the datum scheme changed. 3 weeks of emails between them, and my launch date has not moved. Mar 1 Quote was $41.20/unit - invoice landed at $49.80 12 An expedite fee for the bearing shortage, a repack line, and a test charge that was supposedly always extra. That is $21,500 off the program on one release. Who carries that? Feb 22 Where is my order? - day 18 of silence 24 Eighteen days since the last word. Five emails into the thread and nothing back. These units feed my install crews in 2 weeks, and I am out of ways to tell them we are still waiting. Feb 15 Wrong hand packed in 300 sealed cartons 9 PINNED Receiving opened 3 cartons at random and found left hand bracket assemblies packed under the right hand part number. Now every carton gets opened, and the line is pulling stock by hand. 4:47 PM
This is where the chasing stops. One accountable team. Drawing to dock.
Every handoff, every child part lot, every torque and leak record, every partner selection, every tooling milestone, every customs filing sits with one accountable team on our side. That is the entire reason VIA INDIGOS exists.
Tired of chasing 13 suppliers for 1 assembly?
Send us your BOM and drawings. We send back a full landed cost, a build plan, and one named contact on your assembly program.
Submit RFQ →

YOUR MECHANICAL ASSEMBLY PROGRAM, DE-TANGLED.

A multi part assembly is not one sourcing problem, it is 13 of them running at once. One BOM can carry castings, forgings, CNC machined parts, stampings, rubber parts, springs, and fasteners, each on its own clock. We built VIA INDIGOS so all of it runs as one accountable team. Assembly benches in 6 Indian cities, drawing child parts from a 470+ facility audited partner network spanning 22+ cities, with fixtures and tooling under one roof. One build schedule, one status update, one PO. Whether your volume is 500 units a year or 200,000, we set up the program the same way.

Differential Assembly 23 parts - Ludhiana - torque logged
Gear Sub Assembly Stock 20MnCr5 - Pune
Housing Sub Assembly Tray A356 + bearings - Coimbatore
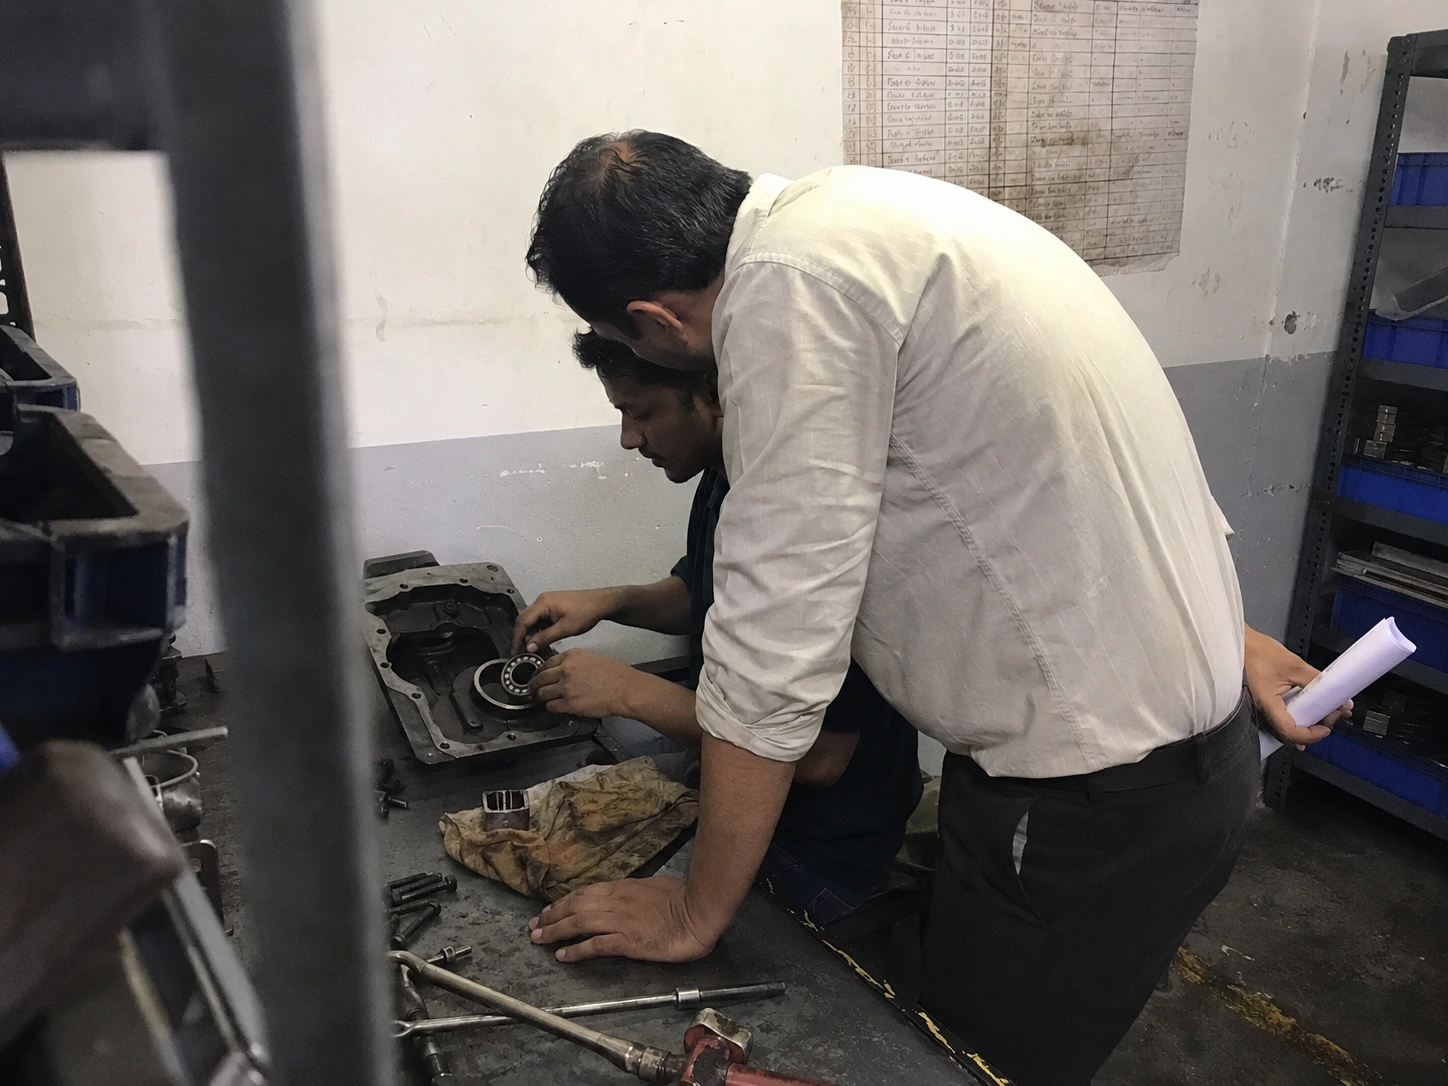
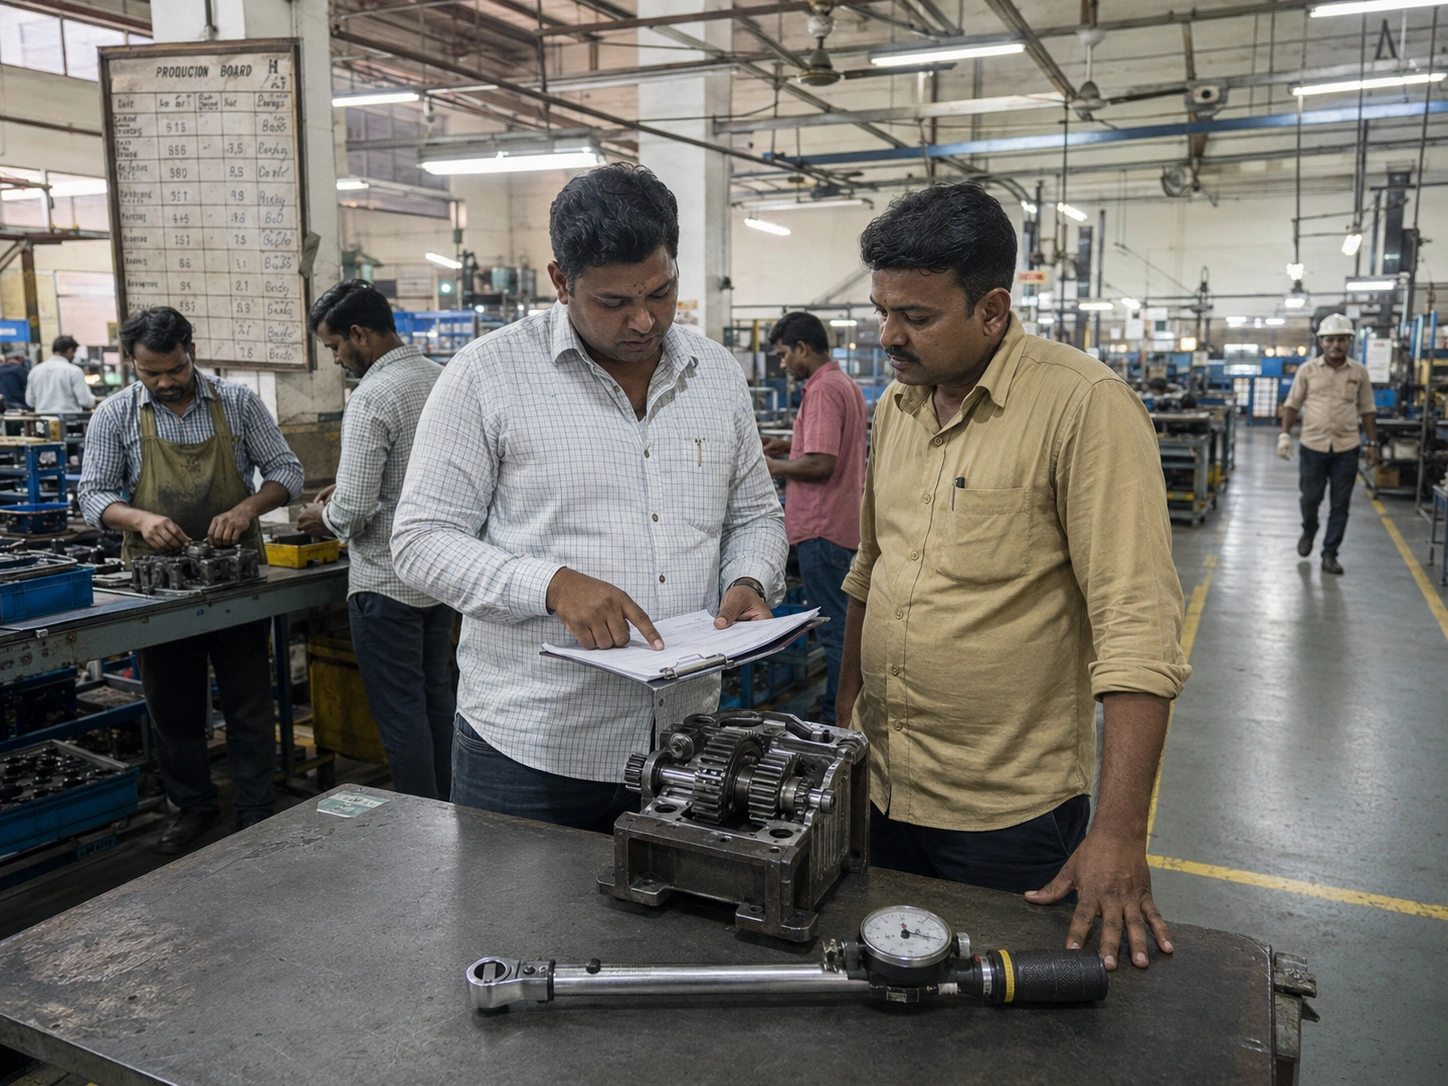
Our engineer reviewing the torque record sheet with the assembly supervisor at our India partner facility before the first PO
Before the first PO
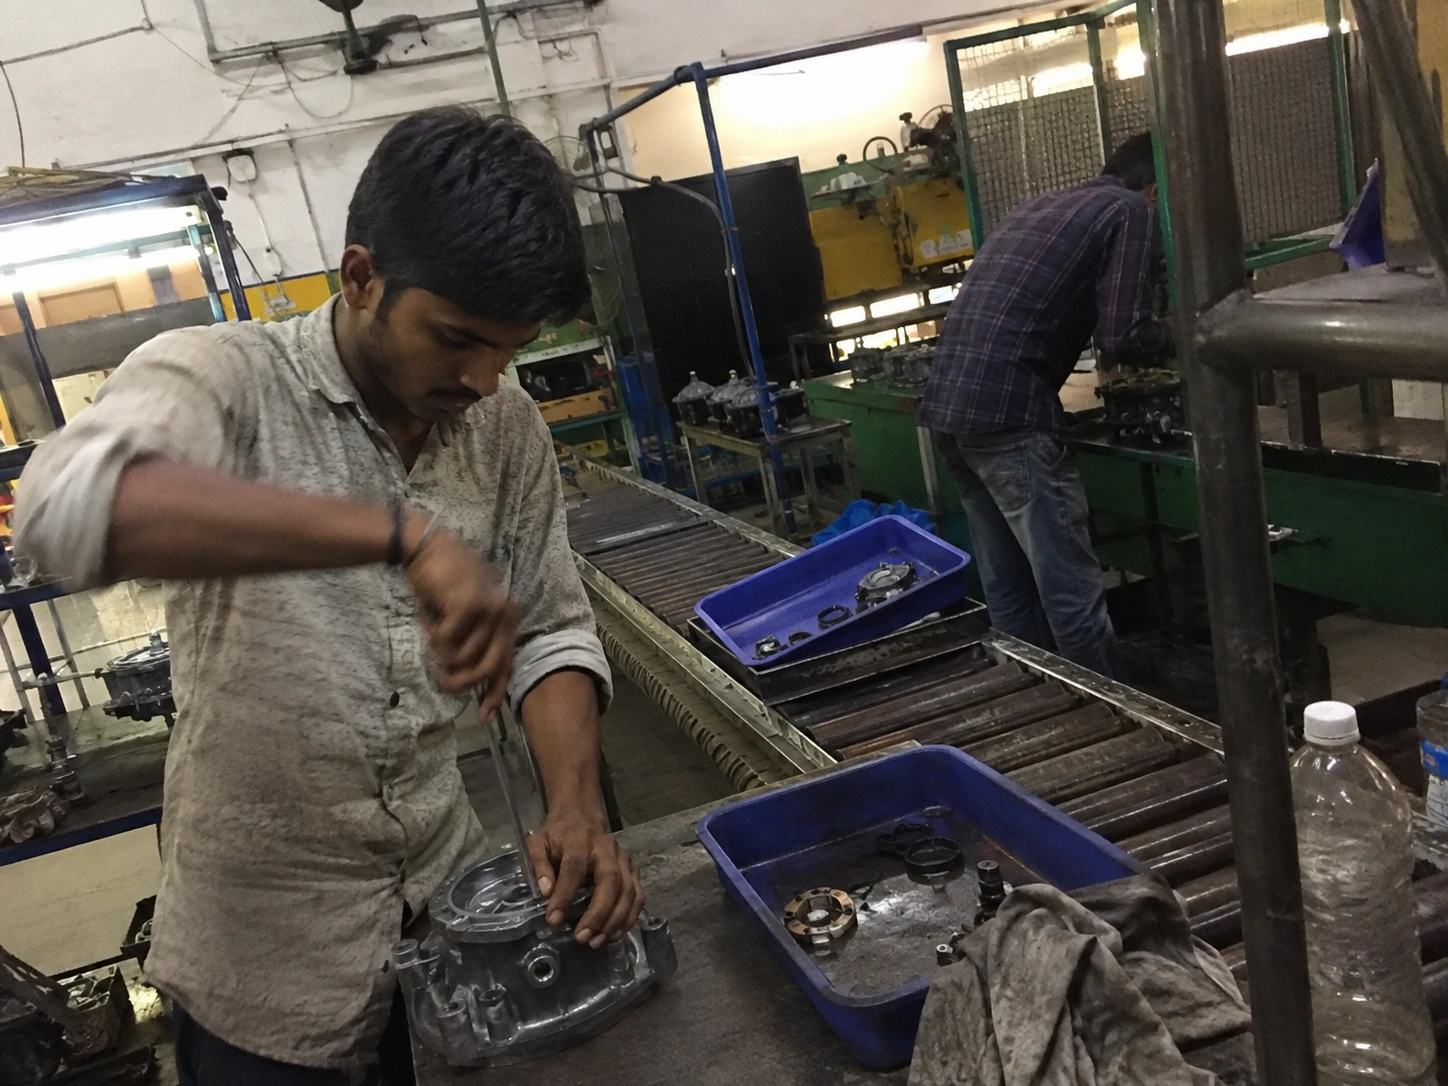
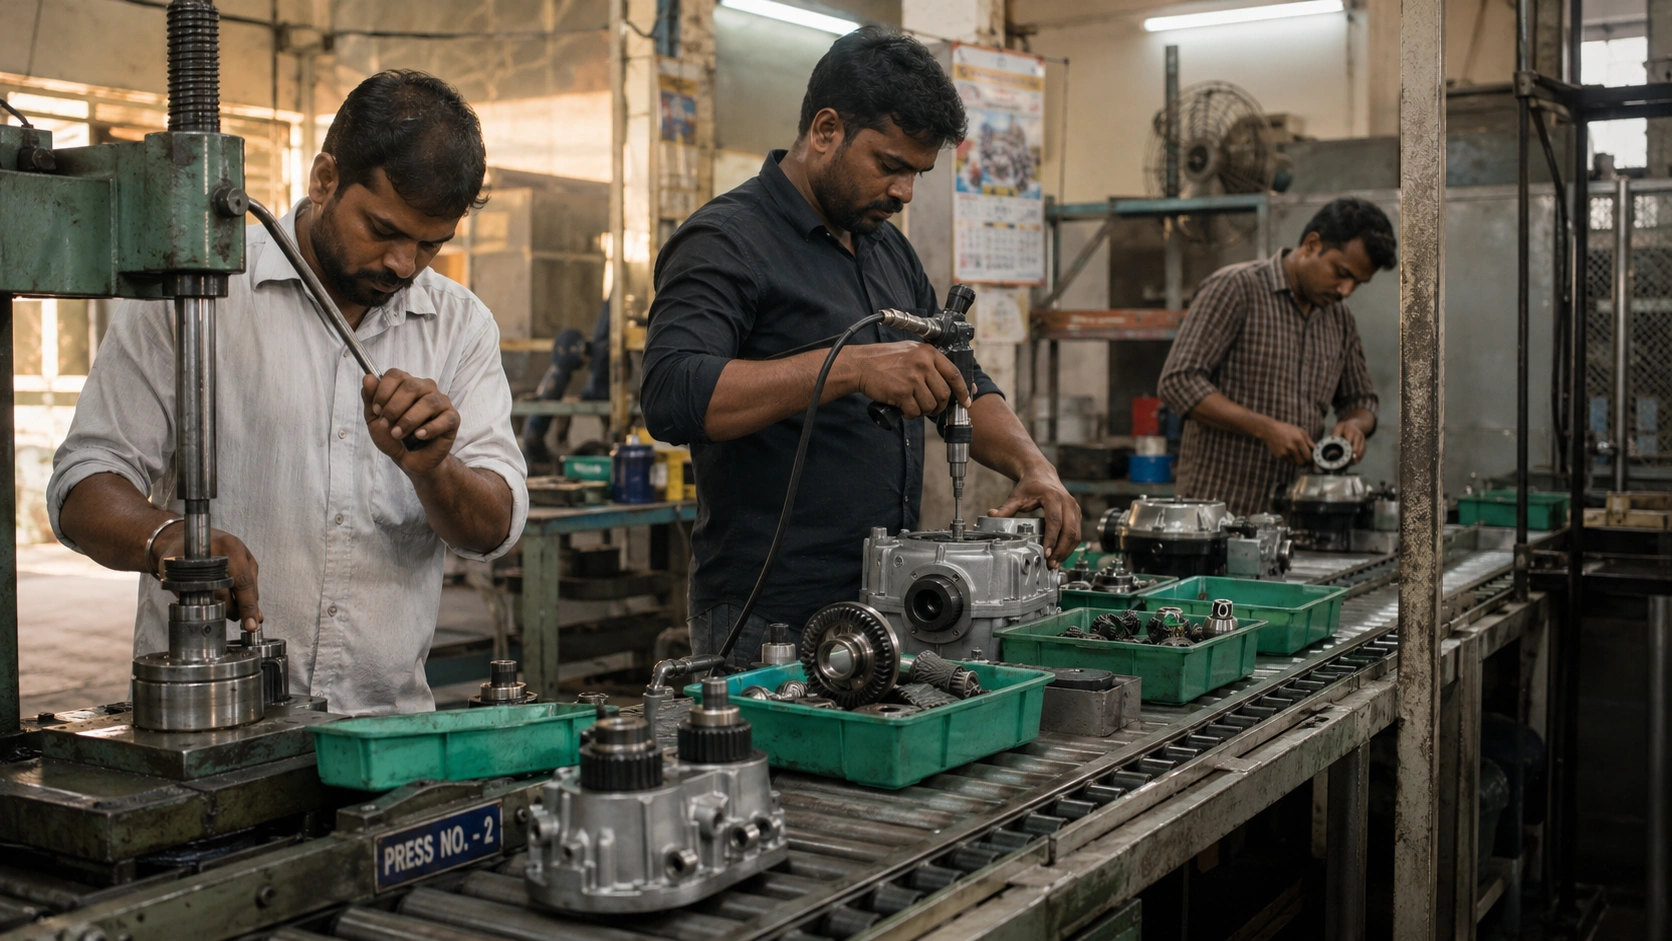
Assembly technicians building gear units at press and torque stations during a production run at our India partner facility
After production starts
Before the first PO

I walk the assembly cell before a single PO is placed. We check the benches, the DC torque tools and their calibration certificates, the press fit stations, the test rigs, and the traceability system that ties a serial number to its child part lots. Then we walk the child part suppliers the same way, foundry to fastener shop. DFM and BOM scrub happen before any tooling is cut. First article builds come with torque logs, test results, photographic evidence, and a written verdict from our quality lead. Boots on the ground, every step of the way.

After production starts

My team runs a shortage board on every open build, so the slowest child part is named on Monday, not discovered on Friday. We track torque values per critical joint, leak test results per serial, first pass yield at the bench, and build rate against your delivery date. You get a status report every Friday covering child part WIP, kit readiness, test results, and shipping milestones. Carton and container loading photos reach your inbox before the seal goes on. Every serial traces to its child part lots and its torque record. We do not wait for you to ask. We report because that is how an assembly program should run.

Where the chain breaks.And where we hold it.

On an assembly, the chain is longer and the breaks multiply: 13 sub suppliers means dozens of chances to drop the ball. We hold every one. Ten real stages, drawing to your dock. No sub-step skipped, no handoff left to chance.

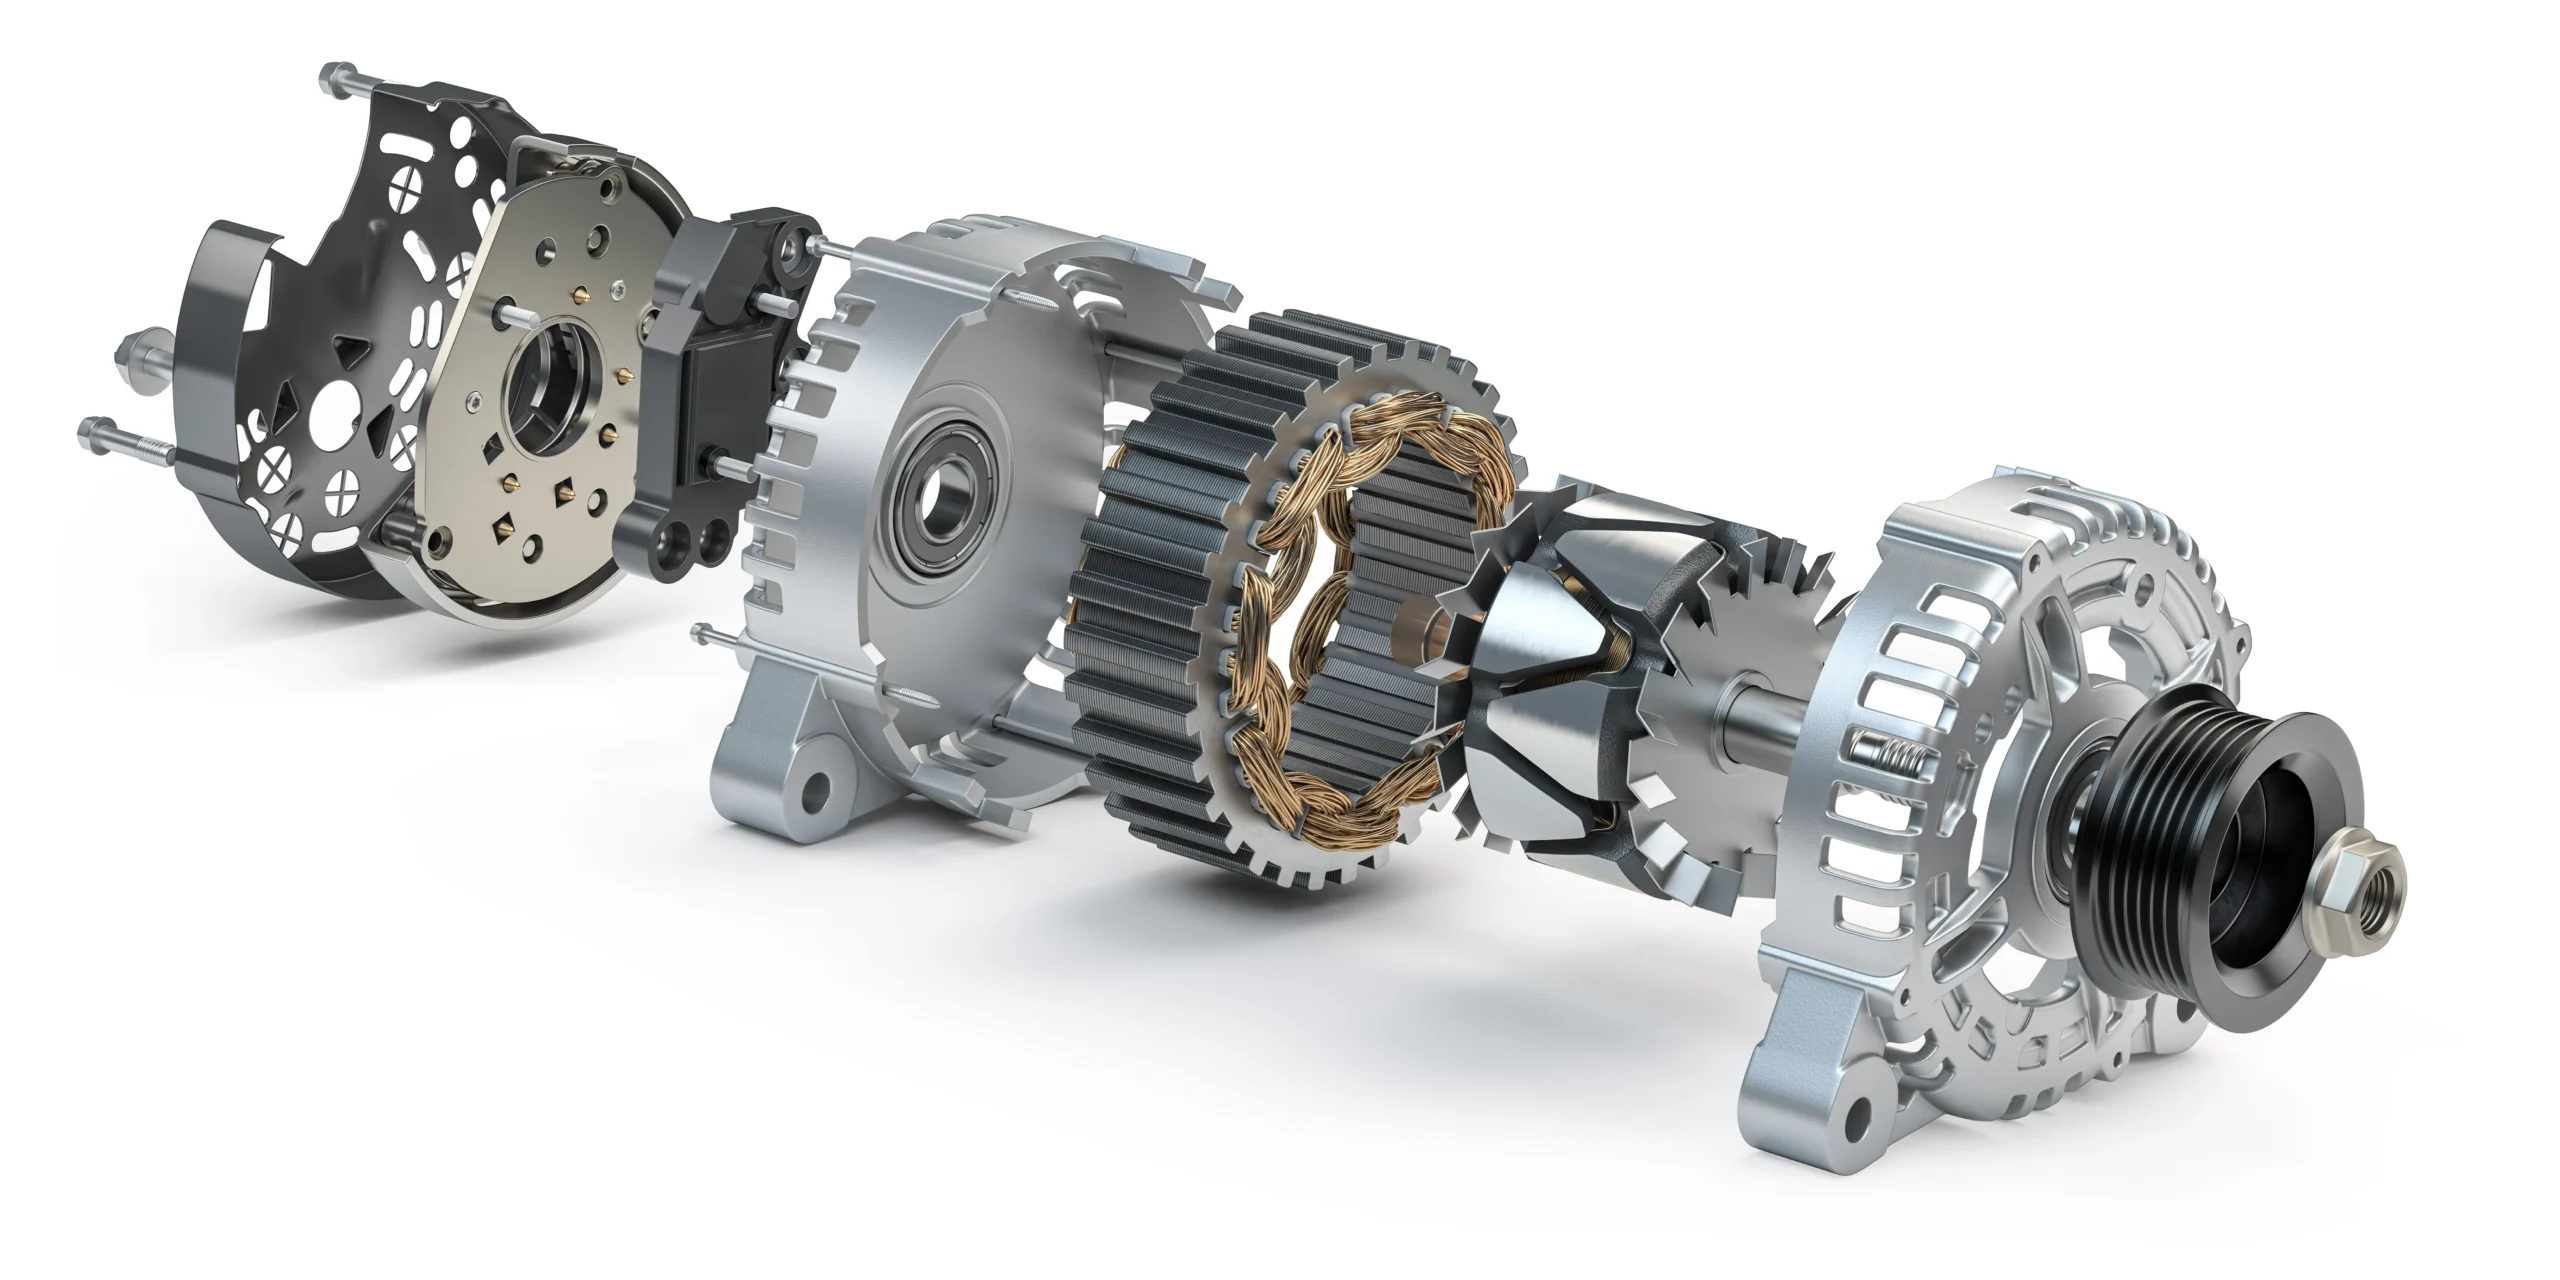
Exploded view of an automotive alternator assembly showing every child part one VIA INDIGOS build brings together
01
Drawing + BOM intake
Break. Most suppliers quote the assembly without reading the BOM. Missing fastener specs and revision gaps surface at the bench.
Hold. BOM scrubbed line by line inside 48 hours. Every child part sourced, priced, or flagged in writing.
02
Quote + landed cost
Break. You get 13 separate quotes and nobody totals them. Duty, freight, and test charges arrive later and break the budget.
Hold. One number per assembled unit, with child parts, fixtures, testing, freight, duty, and inland all built in.
03
PO + program kickoff
Break. Kickoff drifts two weeks while each shop still confirms specs, and your schedule slips on day one.
Hold. Kickoff call inside 5 days of the PO, with the build schedule, sign offs, and names locked in writing.
04
Child part sourcing + tooling
Break. Every child part supplier starts on their own clock. The slowest one quietly sets your delivery date.
Hold. One build schedule. Every child part and tool tracked weekly against the same assembly date.
05
First article build
Break. Parts meet a bench for the first time in production. Stack up and fit problems are found at unit 1 of 5,000.
Hold. Complete FAI units built, measured, torqued, and function tested before production is released.
06
Incoming + kitting
Break. A superseded revision slips into the bins and is found at station 3, half built into 200 units.
Hold. Incoming inspection on every child part lot. Kits staged per unit with a traveler and revision check.
07
Assembly + torque control
Break. Torque set by feel and never recorded. The warranty claim lands on you 8 months later.
Hold. DC torque tools with logged values on every critical joint. Calibration certificates on file.
08
Functional test
Break. Assemblies ship on dimensional checks alone. The leak reaches your customer before it reaches a test rig.
Hold. Pressure decay, hydraulic leak, and function checks per the control plan. Results recorded per serial.
09
PPAP + quality release
Break. PPAP turns up half done with the child part records missing, and production gets released on a verbal nod.
Hold. Assembly level PPAP Level 3 with child part PPAPs rolled in. PSW signed by buyer before a single unit ships.
10
Customs + US delivery
Break. Wrong HS code, a duty surprise on the invoice, and demurrage running before anyone notices.
Hold. HS code locked at the quote, broker briefed, and container photos sent to you before the seal goes on.
Ten handoffs - One accountable team - Drawing to dock.
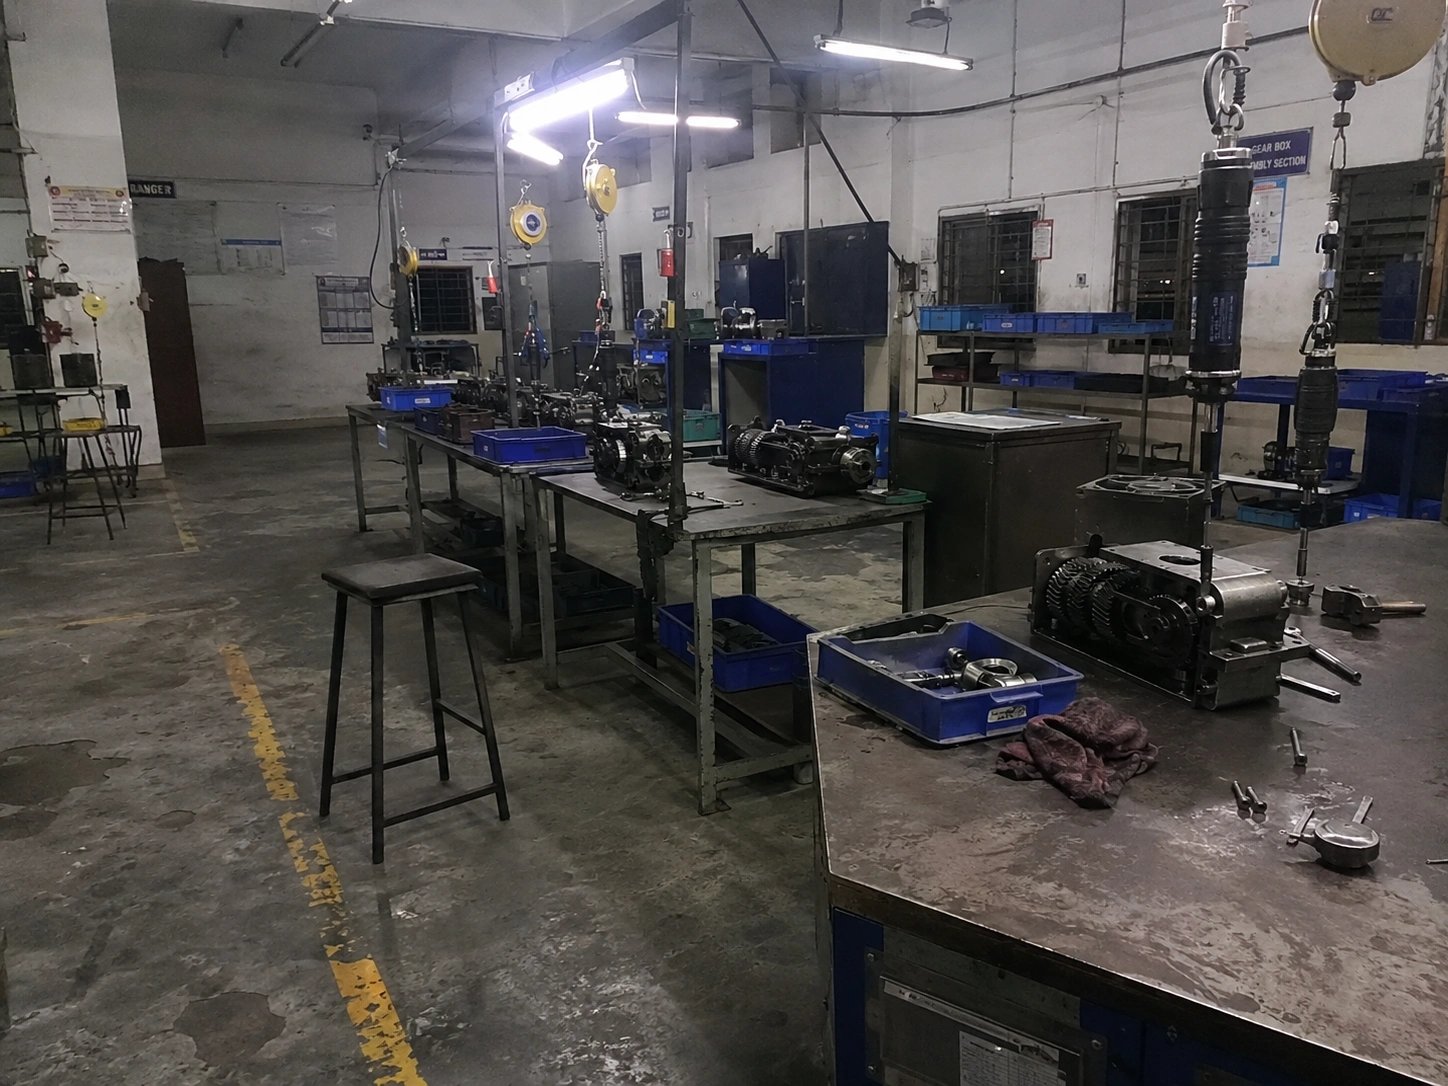
Assembly benches with hanging torque tools and part trays after the shift at our India partner facility

What we do not doon a mechanical assembly program.

We are not a marketplace. We do not match you with a supplier list and call it done. Every partner on your assembly, from the foundry to the fastener shop to the bench, is selected, audited, and managed by our team on the ground in India.
We do not hand you a quote and disappear. From BOM intake through dock delivery, one accountable team stays on your program. Every handoff is documented. Every Friday status update is sent without you asking.
We do not bolt together parts we have not inspected. Every child part lot passes incoming inspection against its drawing and revision before it reaches the bench. Our team audits the cell, the torque tools, the test rigs, the fixture shop, and the people before a single PO is placed.
We do not use your drawings, BOM, or specs to build for anyone else. Your design stays your design. Your tools and fixtures stay yours. Ownership transfers to you on full payment, in writing.
We do not promise a test without a record. Torque values logged per critical joint. Pressure decay and leak results recorded per serial. Salt spray per ASTM B117 where the finish calls it. If we cannot show it, we will not ship it.
We do not claim to own the benches. We own the outcome. The serial trace, the Friday update, the PPAP package, and the tested unit landing on your dock on time. That is the whole job.

Inside our Indiamechanical assemblynetwork.

6 assembly cities. Assembly benches drawing child parts from a 470+ facility audited partner network across 22+ Indian cities. Hover any marker to see partner count and what runs there.

Faridabad 4+ partners
Assembly hub - brake and hardware kits - stamping cluster
Ludhiana 3+ partners
Fastener and machining cluster - gear and spindle builds
Rajkot 3+ partners
Casting cluster - pump and valve assemblies
Pune 4+ partners
Auto tier assemblies - gearbox builds - test rigs
Coimbatore 3+ partners
Pump and motor assemblies - foundry cluster
Chennai 3+ partners
Auto OEM tier - port hub - final builds and export pack

6 assembly cities  ·  470+ facility network  ·  22+ cities behind every BOM

On the assembly bench floorbefore you ask.

Most India sourcing is run from a laptop in Cincinnati. Ours is not. Our team is physically present at partner facilities for first article builds, torque audits, leak test sign offs, and production launches. When a child part slips, we see it before you do. When quality holds, we have the photo evidence to prove it.

Assembly benches in 6 Indian cities, backed by a 470+ facility audited network across 22+. Real people on the floor making sure your BOM becomes a tested assembly that passes PPAP the first time.

Our engineer watching a technician seat a bearing at the assembly bench during a facility visit in India
Assembly technicians pressing bearings and torquing housings at numbered stations on the build line at our India partner facility
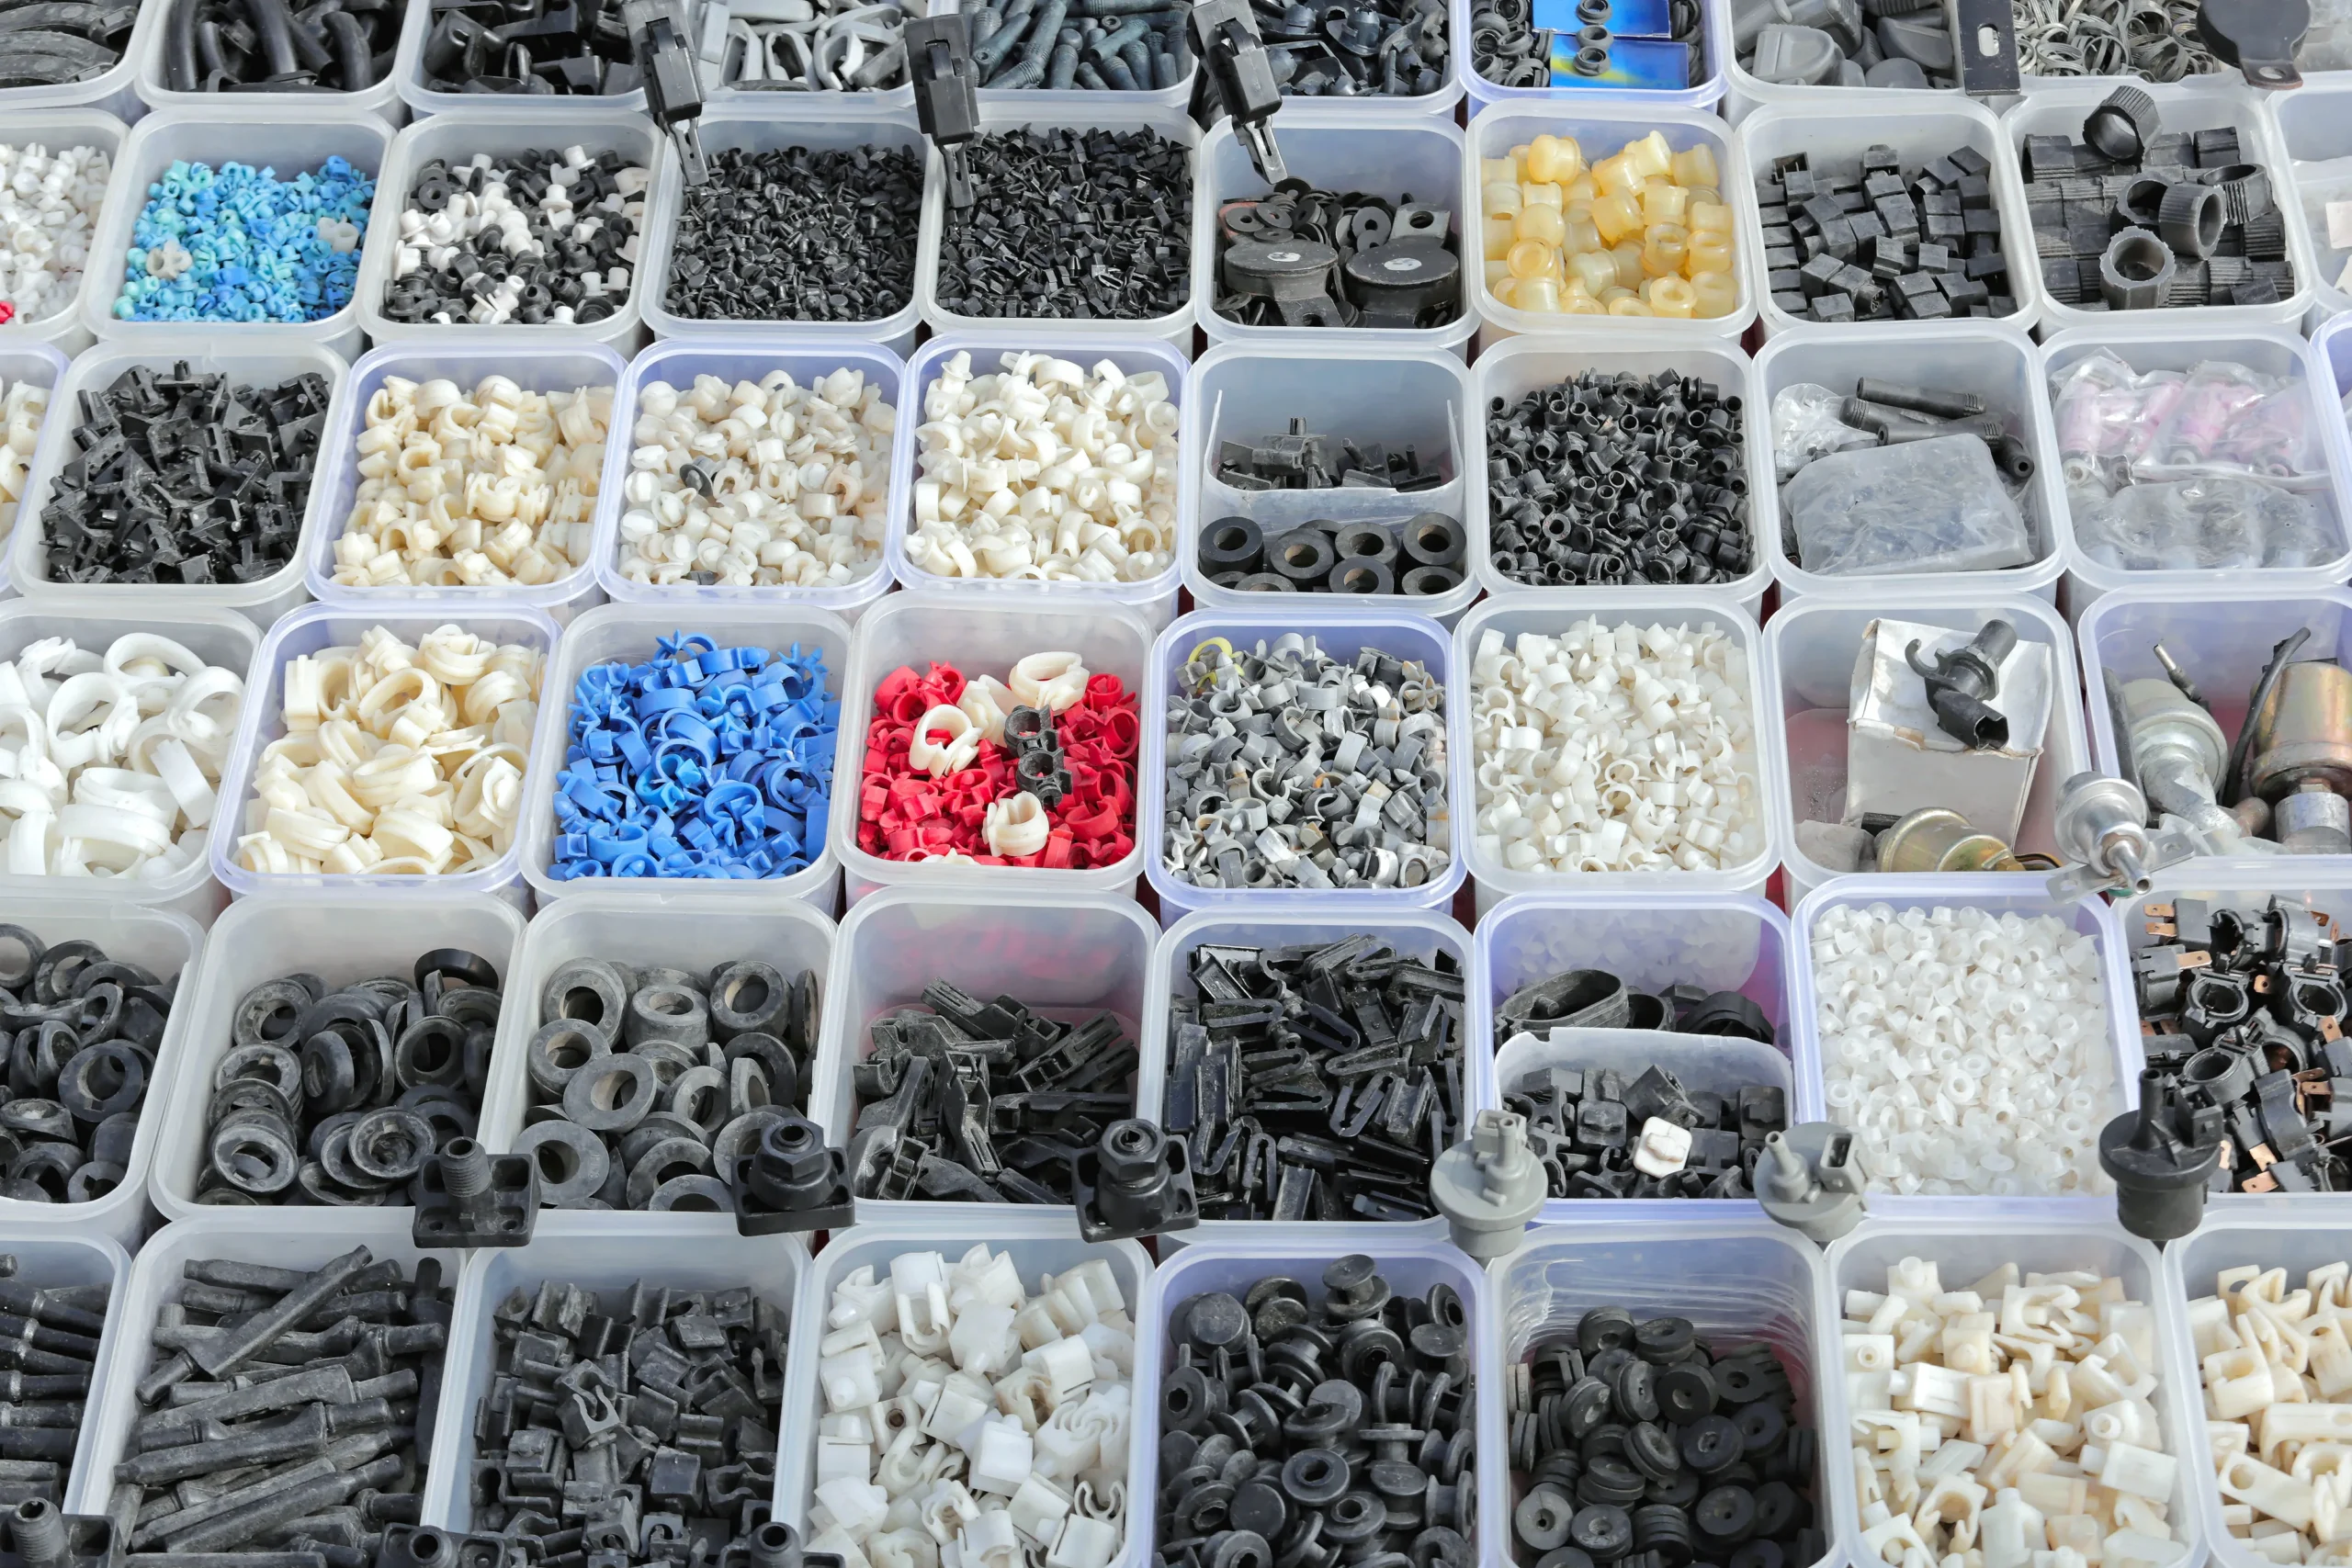
Kitting bins of sorted fasteners, seals, and small child parts staged for one assembly build at our India partner facility

HOW WE CONTROL ASSEMBLY QUALITY.

If a metric does not have a name against it, a target, and a data source, it is not a metric. Below is the scoreboard we run on every assembly program, refreshed weekly, surfaced in your Friday status email.

Submission
Level 3
PPAP every program
Full PSW with capability studies, MSA, and dimensional report.
First pass
≥ 95%
FPY at PPAP
Parts accepted at first submission divided by parts submitted.
On time
≥ 98%
OTD to dock
Promised date versus delivered date at customer dock.
Defect rate
< 500 ppm
Escaped defect
Buyer incoming inspection rejects per million assembled units shipped.
Capability
Cpk ≥ 1.67
Critical joints
Process capability on every customer flagged critical dimension and torque value.
Cost of poor quality
< 1%
COPQ of spend
Total scrap, rework, returns, and warranty claims as percent of program spend.
Traceability
100%
Serial to child lot
Every serial number traced to its child part lots, its torque record, and its test result.
Function testing
100%
Test per serial
Pressure decay, hydraulic leak, and function checks per the control plan. Salt spray per ASTM B117 on coated builds.

FIVE ASSEMBLY STATIONS
WE RUN FROM INDIA.

Follow one build through the 5 stations that turn a crate of child parts into a tested, packed assembly. All of it runs through one VIA INDIGOS playbook. One accountable team from drawing to dock. One status update every Friday. One India network of 470 plus audited partner facilities behind every BOM.

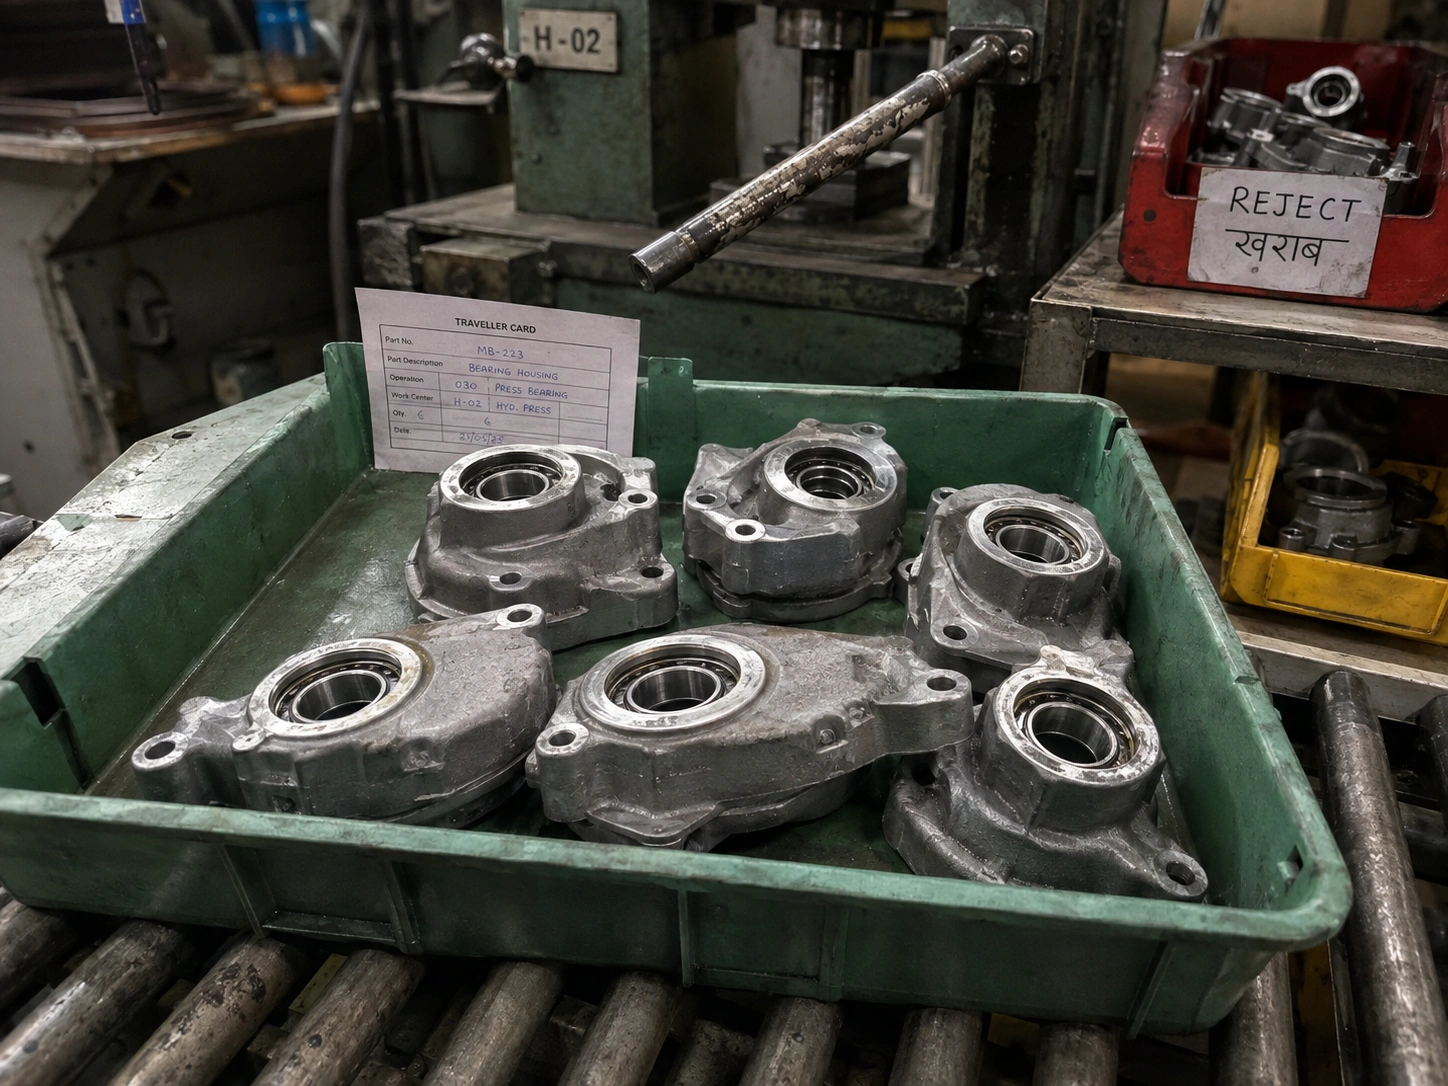
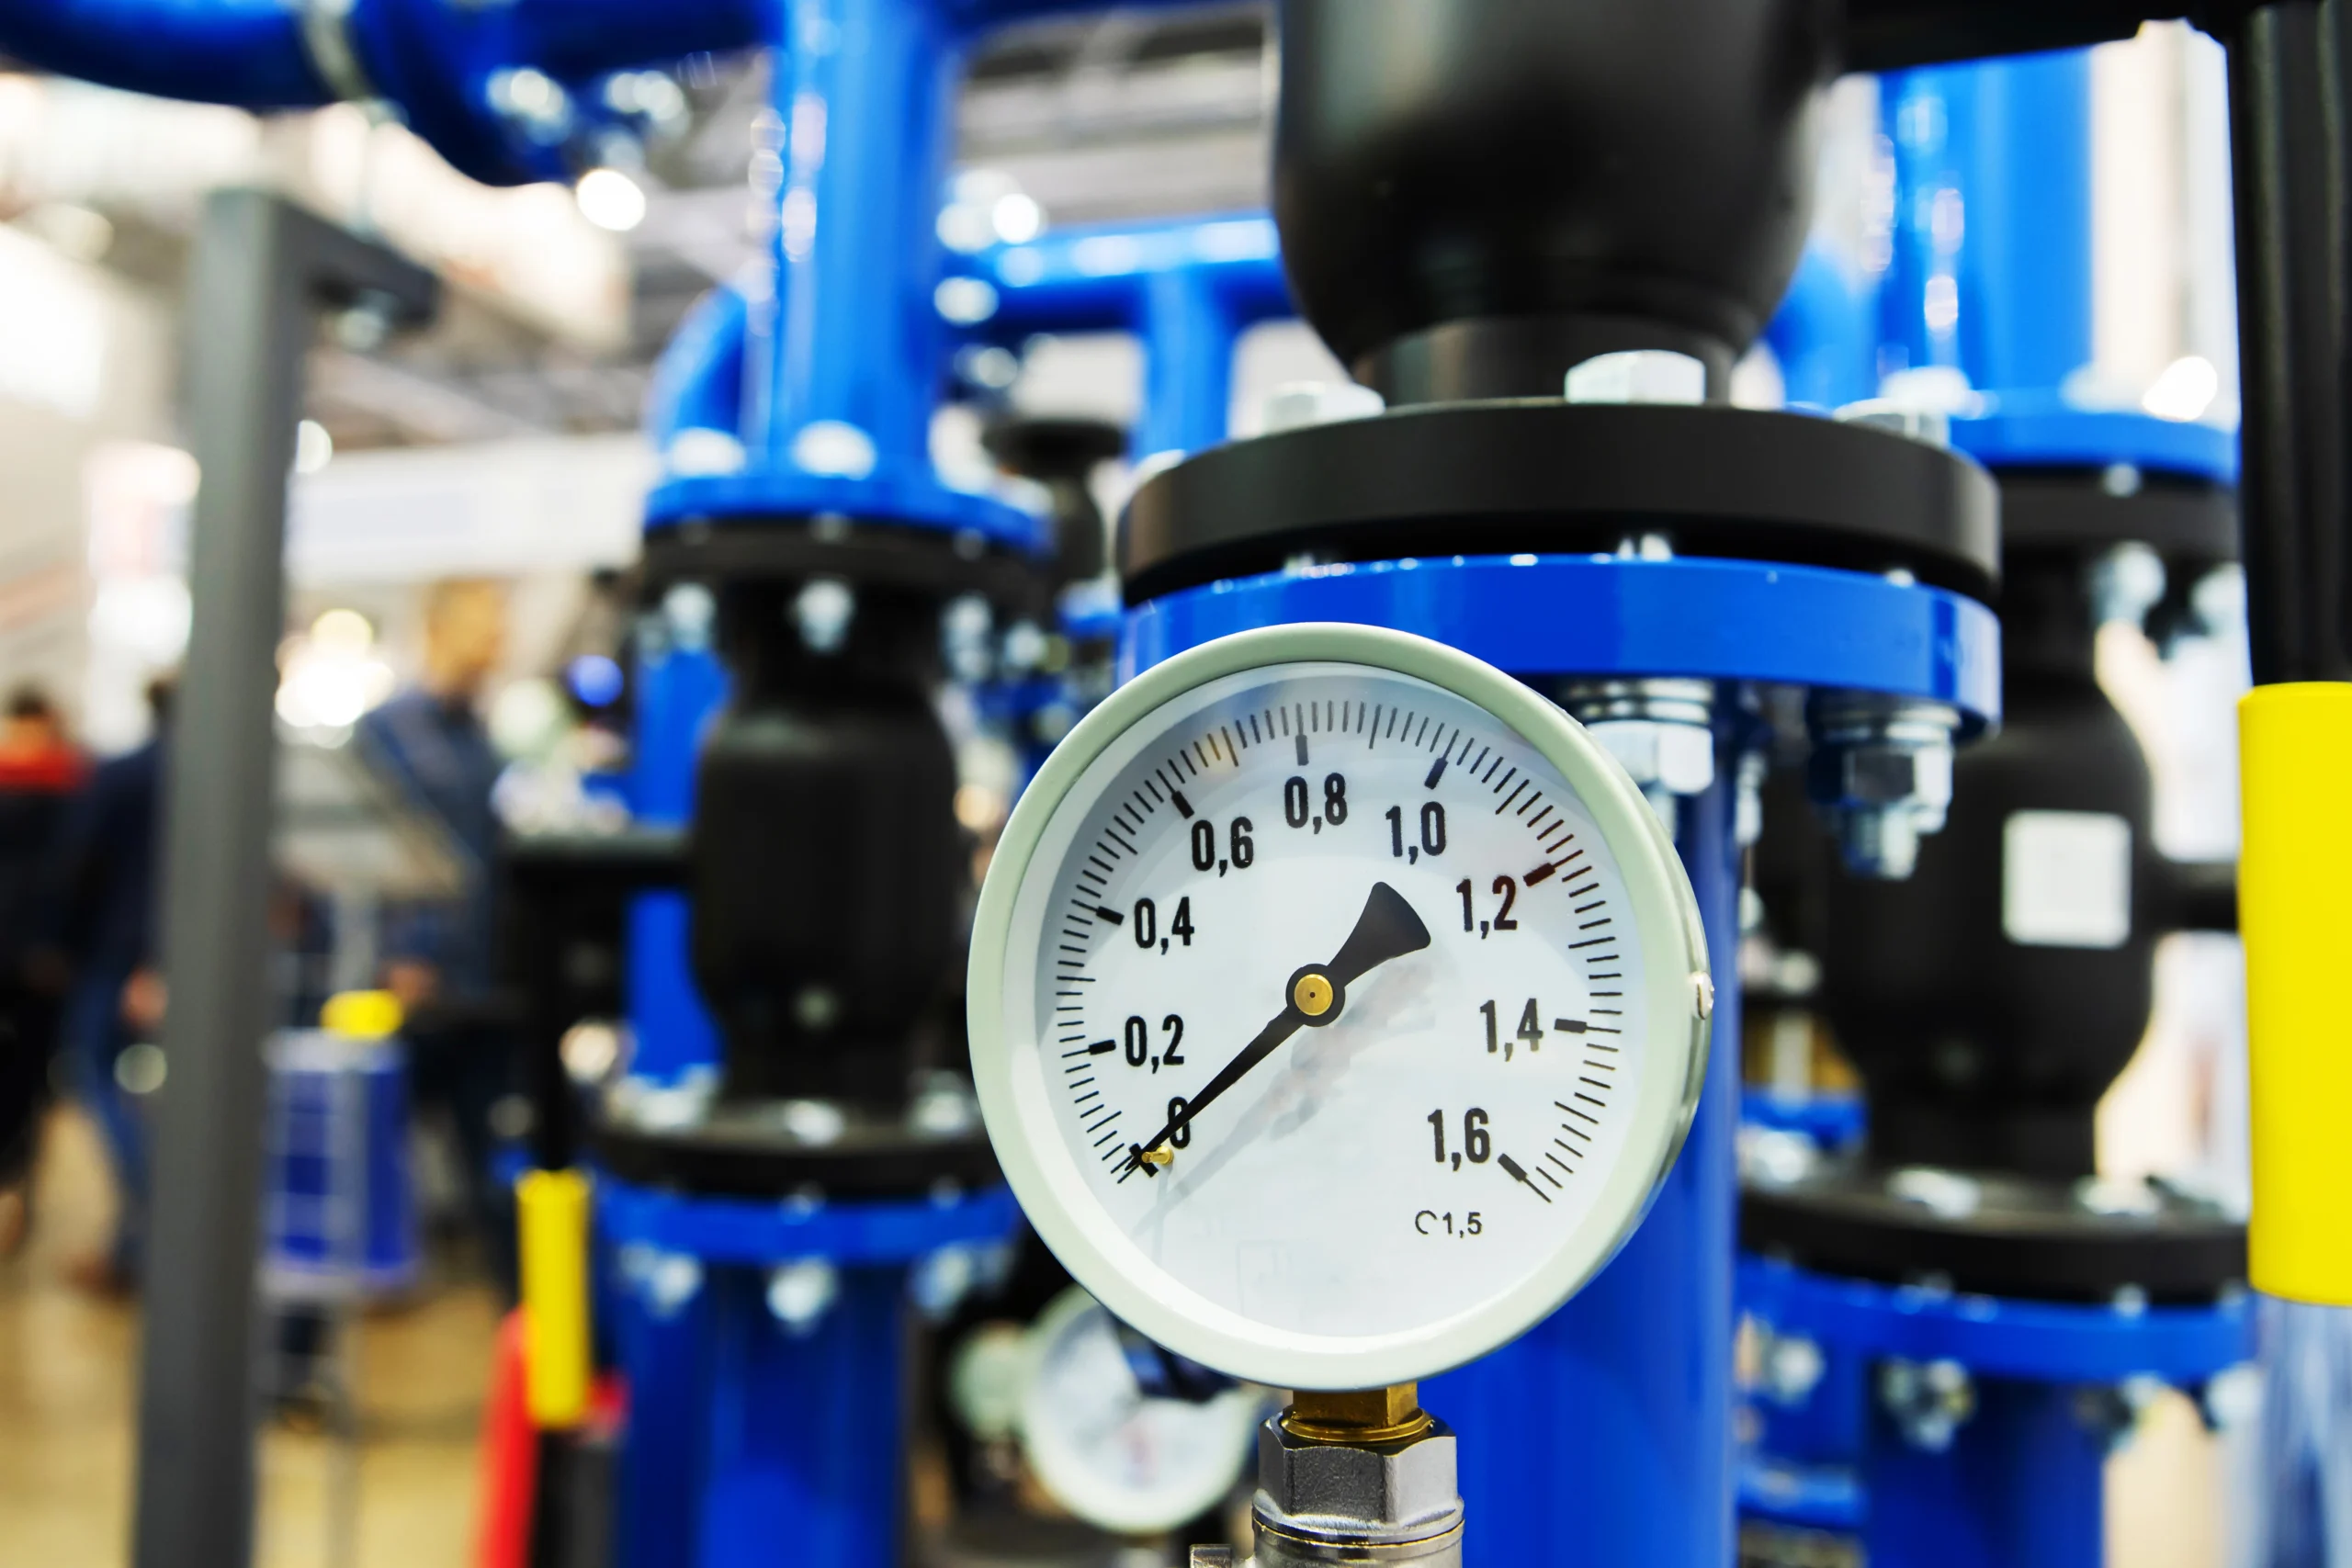
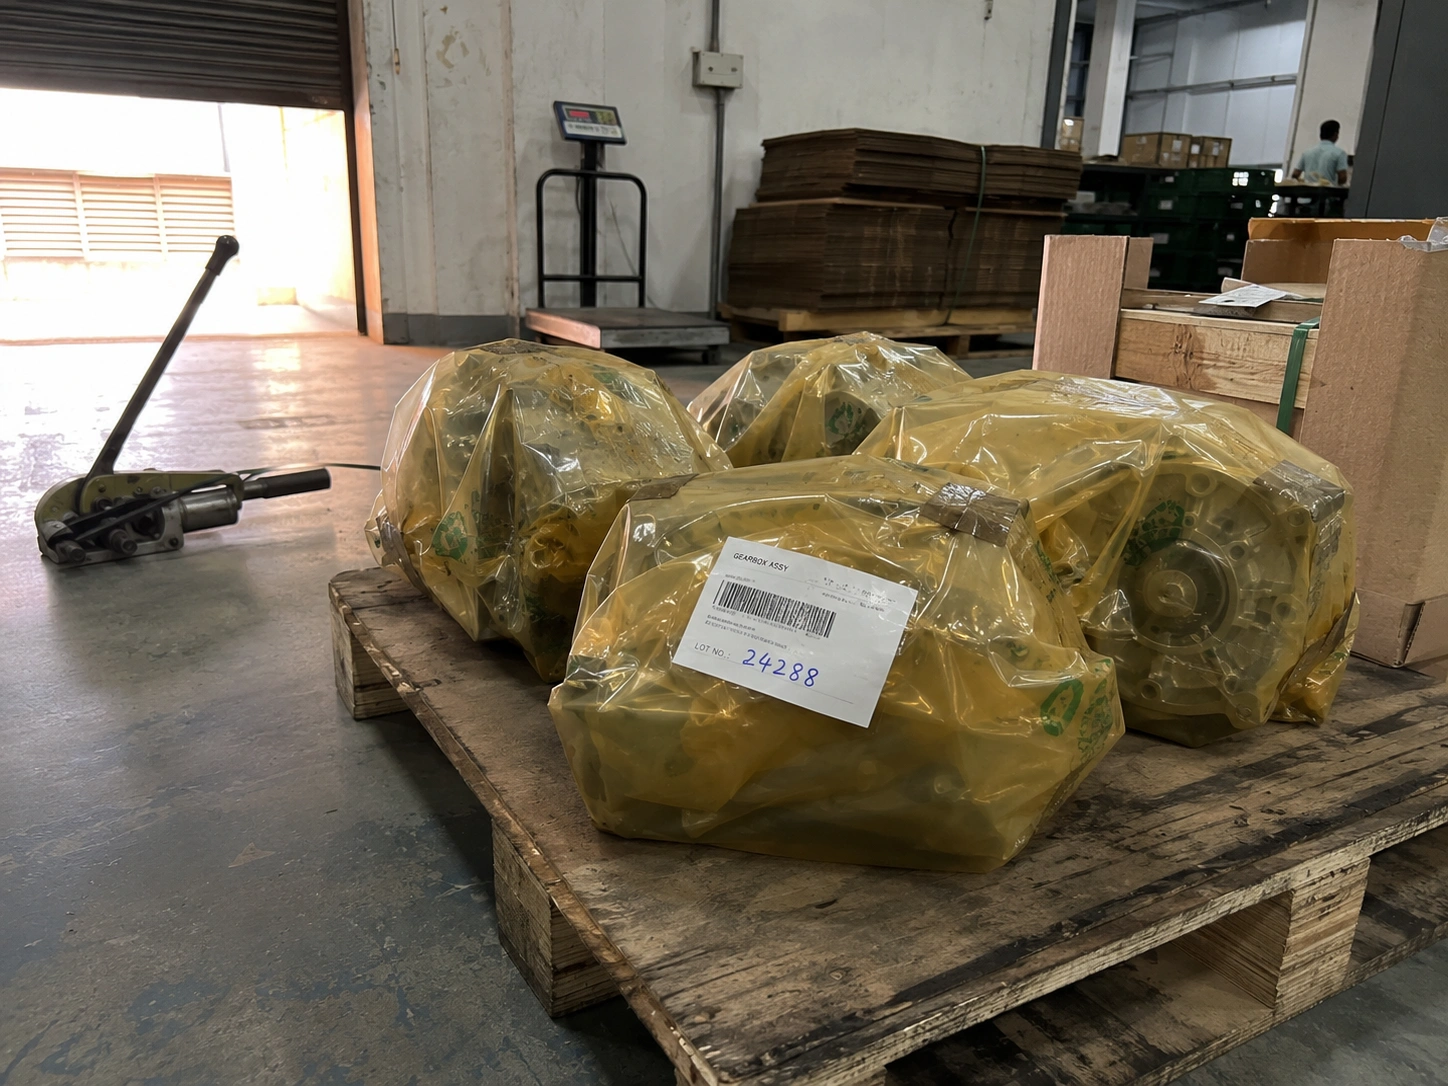
Sorted kitting bins holding fasteners, seals, and small machined child parts staged per build at our India partner facility Cast aluminum housings with freshly pressed bearings in a tray between assembly stations at our India partner facility Technicians building gear housings at press station 2 with torque tools on the assembly line at our India partner facility Pressure gauge reading on the hydraulic leak test rig during a pump assembly test at our India partner facility Completed gearbox assemblies wrapped in VCI paper with lot labels stacked on the dispatch pallet at our India partner facility
01
Incoming + kitting

Incoming inspection and kitting

Every child part lot is inspected against its drawing and BOM revision before it earns a bin. Kits are staged per unit with a paper traveler, so the bench never guesses which revision it is holding and a superseded part cannot reach station 3 half built into 200 units.

Parts per build
up to 38+
Processes
7 in 1 BOM
02
Sub assembly

Sub assembly and press fitting

Bearing pressing, bushing insertion, riveting, and staking on monitored presses, with force and distance watched so a cocked bearing is caught at the press, not at the endurance rig. Each sub unit carries its own trace so the final build inherits a clean history.

Press fits
force monitored
Trace
per sub unit
03
Final assembly

Final assembly with torque control

Every critical joint runs on a DC torque tool with the value logged against the serial, held to plus minus 10 percent of the target. Calibration certificates stay on file per tool. When a warranty question lands 8 months later, the torque record answers it in one email.

Torque
±10% logged
Coverage
every critical joint
Child part machining range
04
Functional test

Leak, pressure, and function testing

Pressure decay for sealed systems, hydraulic leak tests under working pressure, vacuum function checks, and endurance cycling where the control plan calls it. A dimension can pass and the assembly can still leak, which is why results are recorded per serial, not per lot.

Leak
pressure decay
Records
per serial
05
Pack + dispatch

Packing and dispatch

Finished units in VCI wrap with custom foam or partitioned cartons, labeled with your part number, serial, and lot. Cartonization is planned at quote so the pallet that lands feeds your line or your warehouse racks without a repack, and loading photos go out before the seal.

Pack
VCI + custom foam
Labels
part · serial · lot

Assembly sourcing comparisoncost, control, lead time.

Full assembly in India vs sub assemblies vs kitted parts vs loose parts on many POs vs US final build on India parts. Five honest comparisons, not marketing claims. Use this to short list before you send the BOM.

DWG 001 · REV A SCALE 1:1

FULL ASSEMBLY IN INDIA

Volume 500 to 200,000units/year
Lead time 8 to 12weeks to first article
BOM depth up to 38+parts, 7 processes
Testing Per serialleak + torque logged
Fixtures LOW
Pick this when

Recurring volume, many child processes, 1 PO wanted.

DRAWNVI ENG CHKDMS UNITSMETRIC
DWG 002 · REV A SCALE 1:1

SUB ASSEMBLIES TO YOUR LINE

Volume 1,000 to 500,000modules/year
Lead time 6 to 10weeks to first article
Scope modulesdrop into your final build
Testing Per modulefunction checked
Fixtures LOW
Pick this when

Final assembly stays on your line, modules arrive tested.

DRAWNVI ENG CHKDMS UNITSMETRIC
DWG 003 · REV A SCALE 1:1

KITTED CHILD PARTS

Volume 200 to 100,000kits/year
Lead time 5 to 9weeks to first kit
Scope 1 cartonper unit, your bench builds
Testing Per child lotincoming inspected
Fixtures LOW
Pick this when

Your bench does the build, you want 1 supplier not 13.

DRAWNVI ENG CHKDMS UNITSMETRIC
DWG 004 · REV A SCALE 1:1

LOOSE PARTS, MANY POS

Suppliers up to 13each on its own clock
Lead time set bythe slowest supplier
Coordination yourschasing, matching, sorting
Testing Per partno build level record
Your admin load HIGH
Pick this when

Honestly, never. This is the status quo we replace.

DRAWNVI ENG CHKDMS UNITSMETRIC
DWG 005 · REV A SCALE 1:1

US FINAL BUILD, INDIA PARTS

Volume 500 to 100,000units/year
Lead time 6 to 10weeks to first kit
Scope kits + subsfinal assembly in the US
Duty angle assembledin USA, parts from India
Fixtures MEDIUM
Pick this when

Tariff or IP reasons keep the final build in the US.

DRAWNVI ENG CHKDMS UNITSMETRIC
Share your assembly project today.
A BOM, a drawing pack, or a sample unit is enough to start. Send what you have and get a real read on child part cost, fixtures, and landed cost.
Submit RFQ →
Build discipline

FAI BUILD . TEST . PPAP .
NO ASSEMBLY SHIPS WITHOUT A SIGN OFF.

Three sign offs, photo evidence at every step. We do not move a build forward unless the sign off before it is closed. An assembly that ships on dimensional checks alone is an assembly that leaks on your customer, and we would rather catch it on the rig than on your line.

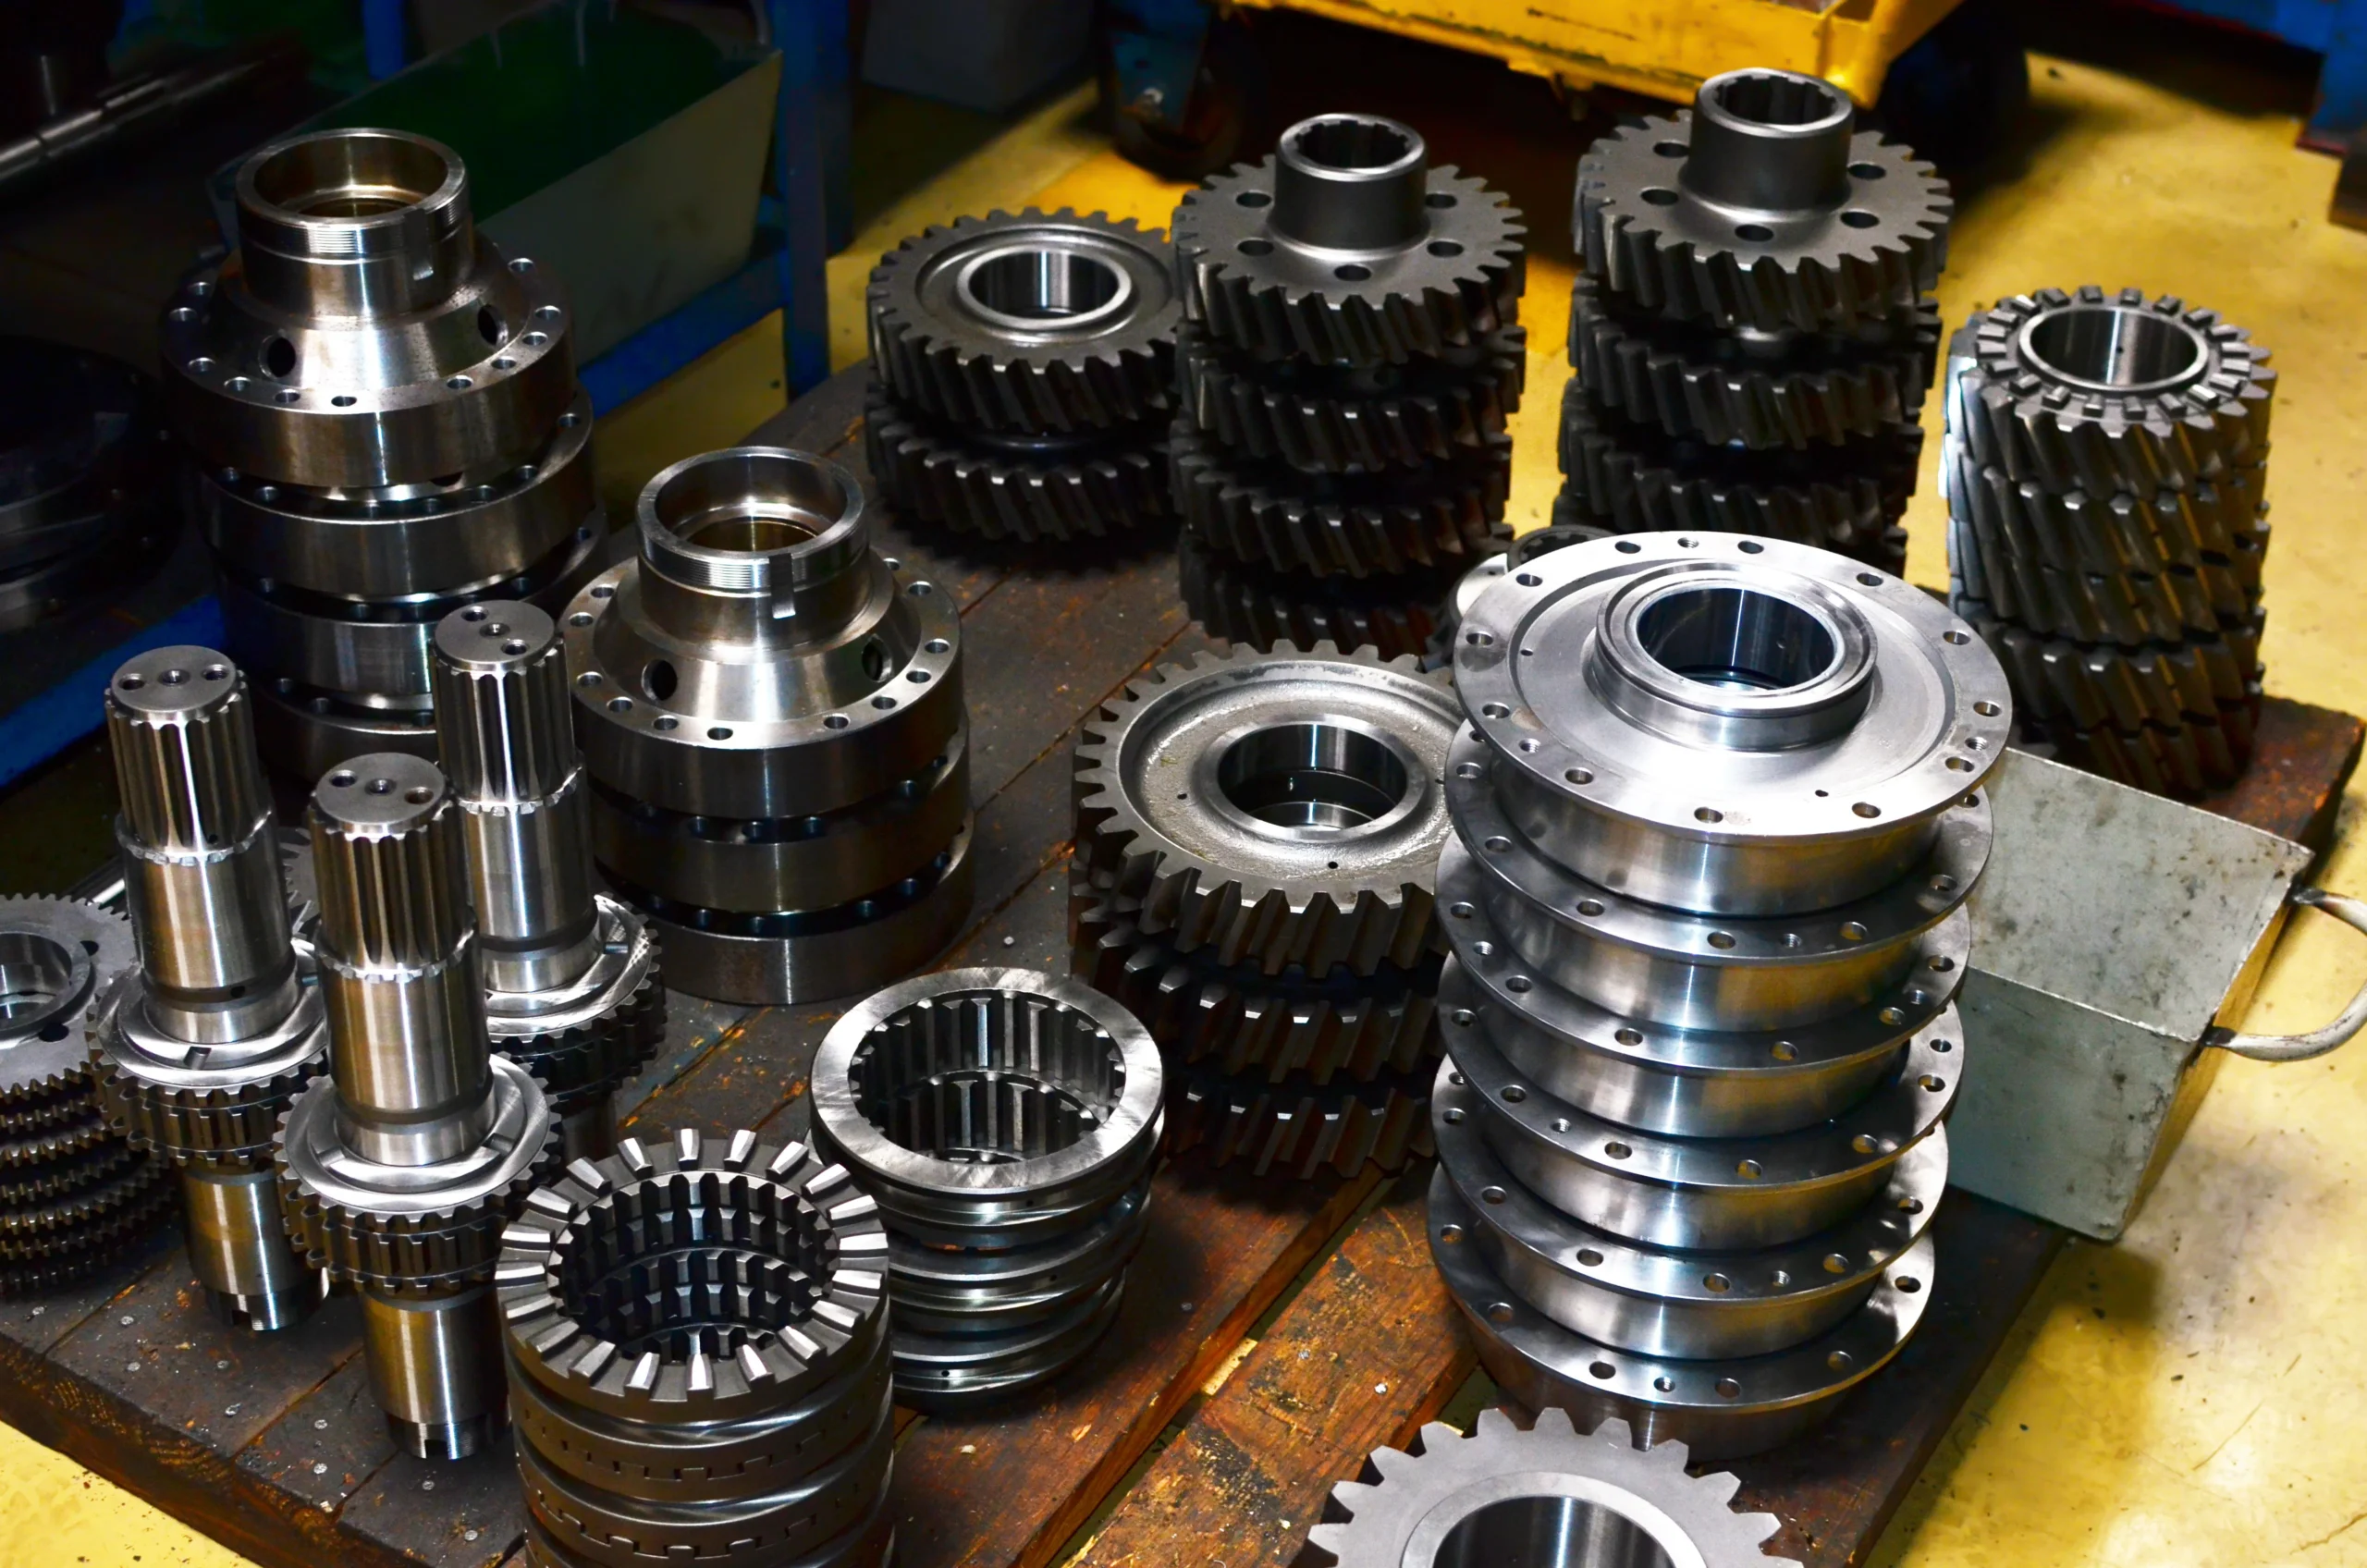
Machined gear clusters and hubs staged on the rack for a first article assembly build at our India partner facility Hydraulic leak test rig gauge under pressure during the functional test sign off at our India partner facility Our engineer and the assembly supervisor reviewing the PPAP evidence and torque records before production release at our India partner facility
Sign off one
First article build

Complete units built from production intent child parts, on the production fixtures, by the production crew. Stack up and fit verified on the bench, every critical joint torqued and logged, every child part checked against its BOM revision. If two parts fight each other, we find it here at unit 1, not at unit 5,000. The build is signed off before production is scheduled.

  • BOM revision verified per child part
  • Stack up and fit check on the bench
  • Torque values logged per joint
  • Photo set archived in the project file
Sign off two
Functional test sign off

The FAI units go to the rig. Pressure decay on sealed circuits, hydraulic leak under working pressure, vacuum and function checks, and endurance cycles where the control plan calls them. Test rig calibration certificates on file. Results reach you per serial before production releases, so the first leak a unit ever sees is on our rig, not your line.

  • Leak and function tests per control plan
  • Torque audit re-check on tested units
  • Test rig calibration certificate on file
  • Buyer engineering call before PPAP
Sign off three
Production sign off

PPAP Level 3 at the assembly level, with child part PPAPs rolled into the file. PSW signed by the buyer. Capability studies above Cpk 1.67 on critical dimensions and torque values. Serial traceability live to child part lots. Production releases only after the buyer has the full package in hand.

  • Assembly level PPAP Level 3 signed off
  • Child part PPAPs rolled into the file
  • Cpk above 1.67 on critical joints
  • Serial to child lot traceability live
What one build carries

One assembly BOM.38 parts, 7 processes.

This is what a real gearbox style assembly BOM looks like once you open it: 38+ unique parts, 7 manufacturing processes, 10+ materials, up to 13 sub suppliers. Below is a condensed version of one build we run. Every line carries its own drawing revision, its own incoming inspection, and its own lot trace into the serial record.

Part family Process Material Qty per unit Source cluster
Housing Gravity die casting + CNC A356 aluminum 1 Rajkot
Mounting bracket Closed die forging + machining EN8 steel 1 Ludhiana
Gear cluster Hobbing + heat treat 20MnCr5 3 Pune
Cover plate Sheet metal stamping CRCA steel 1 Faridabad
Seals + O rings Rubber moulding NBR 70 6 Chennai
Bushes Machined bronze SAE 660 4 Coimbatore
Springs Coiling + shot peen EN47 spring steel 2 Ludhiana
Fasteners Cold heading, class 8.8 Zinc plated MS 14 Faridabad

The slowest line on this table sets your delivery date. That is the line our shortage board watches hardest, and the one you hear about on Monday instead of discovering on Friday. Full BOMs, material certificates, and lot traces go in the PPAP file.

Submit your RFQ

Send your assembly drawing pack.
Get a full landed cost.

Upload the assembly drawing, the BOM, and child part drawings. We scrub the BOM, run DFM, and return a full landed cost per unit with build timeline and PPAP scope. You get one contact from intake to ship.


    Drop drawings here or click to browse

    PDF · DWG · DXF · STEP · IGES · IMAGES · UP TO 50MB


    We respond within 24 hours. Your drawings are never shared with third parties. Mutual NDA available on request.

    Same playbook - eleven verticals

    Eleven industries we build assemblies for.

    Every industry has its own certs, its own regulatory pressure, its own drawing conventions. The build discipline stays the same. What changes is the testing and the documentation that move with the assembly.

    Capabilities Beyond Assemblies.

    Mechanical assembly questionswe get every week.

    Plain English answers, written for procurement and engineering teams who want a real number, not a brochure. Last reviewed by Mandeep Singh in August 2026.

    Kitting programs land a first kit in 5 to 9 weeks. Sub assemblies run 6 to 10 weeks to first article. Full assembly programs run 8 to 12 weeks from PO to a signed first article build, because the slowest child part tool sets the date. On one program we delivered a critical sample built across 13 partner floors in 7 weeks.

    If a supplier quotes 3 weeks on a 38 part BOM with new tooling, ask which child parts that timeline actually covers. It is usually the easy ones.

    Assembly level PPAP Level 3 means the buyer gets the full package for the build, not just the parts: signed PSW, dimensional report on assembly callouts, torque and functional test results, control plan covering every joint and test, PFMEA, MSA on the inspection methods, and the child part PPAPs rolled into the same file.

    Production does not release until the buyer has the package in hand and the PSW is signed. That is the discipline. No PPAP, no shipping.

    Builds run up to 38+ unique parts across 7 processes: casting, forging, CNC machining, stamping, rubber moulding, spring coiling, and cold headed fasteners, in 10+ materials, coordinated across up to 13 sub suppliers on one PO.

    The BOM scrub at intake maps every line to a source cluster and a lead time, so the critical path is named before the quote, not after the slip.

    Per the control plan: pressure decay on sealed circuits, hydraulic leak under working pressure, vacuum and function checks, torque audits, and endurance cycling where the duty calls it. Salt spray per ASTM B117 on coated builds.

    Results are recorded per serial, not per lot, so a warranty question 8 months later is answered in one email, with the record attached.

    The MOQ is driven by the child parts, not the bench. Castings and forgings typically run 250 to 1,000 pieces per release, machined and stamped parts less, and kitting programs start from a few hundred units per release.

    Send the BOM and the annual volume, and the quote comes back with the release size that makes the price work per line.

    Default is FOB Nhava Sheva or CIF US West Coast. DDP is available on request with a logistics markup disclosed up front. Inbound preferences are Los Angeles, Long Beach, New York, Newark, and Chicago, with alternates only when they improve lead time or cost.

    For programs with US warehouse pull, we hold finished assemblies or kits and ship JIT to your dock. Storage and handling fees on a published rate card.

    You do. Fixtures, gauges, dies, and molds transfer to the buyer on full payment, in writing, with a tool record per item documenting ID, usage, correction history, and storage location. Tools stay at partner facilities on a bailment basis, available for inspection or transfer at any time.

    If you want to move programs in 18 months, the tools are yours. We do not lock tooling to facilities or hold it hostage.

    Every change runs through a written engineering change loop. The revision lands, the BOM is updated, affected child part suppliers are notified the same day, and the cutover lot is agreed with you in writing. Open stock at the old revision is counted and dispositioned, use up, rework, or scrap, before the new revision releases.

    Kits and travelers carry the revision on paper, so a superseded part cannot reach the bench, and the serial record shows exactly which units carry which revision. No silent cutovers.

    Last call

    Your assemblies are
    worth a free quote.

    Send us your BOM and drawings and judge us as your assembly supplier on the reply. You get a full landed cost per unit, a build timeline, the recommended assembly route, and a PPAP scope. One contact from intake to ship. No commitment required.

    30 minutes · no obligation · bring your drawings · field notes from the floor

    This website stores cookies on your computer. Cookie Policy